Material Innovation: Nanotechnology Spearheads Industrial Transformation
Nanotechnology in Industry is rapidly reshaping global industrial development. Throughout history, major breakthroughs in materials science have driven technological progress, and today nanoscale engineering is opening performance possibilities that were once impossible to achieve. By manipulating matter at the atomic and molecular scale, nanotechnology in industry enables unprecedented control over material properties, making it a key driver of modern industrial transformation.
I. H2: Nanotechnology in Industry: What Happens at the Nanoscale
When materials are structured at 1–100 nanometers, their electrical, thermal, and mechanical properties shift dramatically. Two core effects explain this change.
1. Quantum Size Effect
At the nanoscale, electrons behave differently. Their energy states become discrete rather than continuous.
Therefore, the material’s optical and electronic characteristics change.
This effect supports new progress in optoelectronics, quantum sensors, and miniaturized chips.These effects are fundamental to nanotechnology in industry, especially in optoelectronics, sensors, and next-generation semiconductor manufacturing.
2. Giant Surface Effect
Nanomaterials have a very large surface-area-to-volume ratio.
As a result, they become more reactive and more efficient in adsorption and catalysis.
For example, nanoporous electrodes allow faster charge exchange in next-generation batteries.
II. Industrial Fields Accelerated by Nanotechnology in Industry
Nanotechnology in Industry Applications in Energy & Environment
Nanotechnology does not replace traditional materials—it improves them.This approach highlights how nanotechnology in industry enhances conventional materials rather than replacing them, delivering higher performance with minimal material addition.
A polymer that originally lacked conductivity can become conductive simply by adding small amounts of conductive nanoparticles.
This approach allows manufacturers to tune performance such as:
Thermal and electrical conductivity
Mechanical strength and wear resistance
UV stability and antibacterial capability
Because nanomaterials have extremely high surface efficiency, even 0.2% by weight can significantly change performance.
Therefore, nanotechnology delivers both high efficiency and cost-effectiveness.
III. Industrial Fields Accelerated by Nanotechnology
Nanomaterials are already widely used in polyesters, epoxy resins, polycarbonates, silicones, phenolic resins, gypsum, and many other systems.
When modifying the bulk material is not suitable, nanocoatings can be applied on the surface to provide:
Wear resistance
Chemical stability
UV shielding
Antibacterial protection

For manufacturers, nanomaterials offer a unique competitive edge—delivering added strength, conductivity, or other advanced properties while keeping raw material costs low.
From a broader industrial and research perspective, the rapid adoption of nanotechnology in industry is supported by extensive peer-reviewed studies published in leading journals such as Nature Nanotechnology, which document how nanoscale material engineering enhances performance across energy, electronics, and manufacturing sectors.
Reference: https://www.nature.com/naturenanotechnology
In energy and environment, nano-filtration membranes can efficiently remove micropollutants from water, while nanocatalysts help convert industrial waste gases into useful chemicals—key technologies for sustainable development.
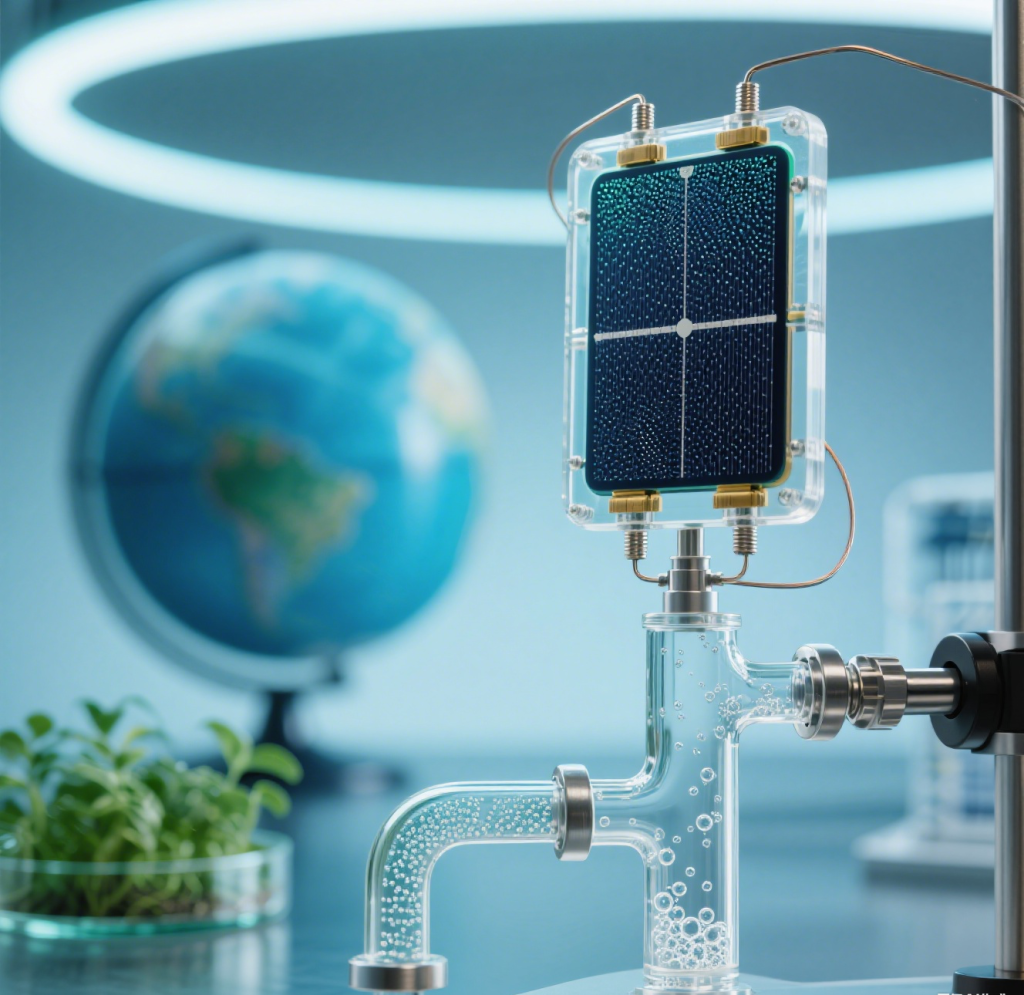

In biomedicine, nanoscale drug carriers enable targeted delivery to disease sites, reducing side effects and improving treatment efficacy.
Conclusion
Nanotechnology in Industry is not merely a future concept — it is already reshaping industrial production, material design, and manufacturing efficiency today. By redesigning materials from the atomic scale, it provides a powerful toolkit for innovation across manufacturing, energy, healthcare, and consumer markets. Moreover, as nanomaterials continue to evolve, their integration with artificial intelligence, smart sensors, and IoT-enabled devices promises even greater efficiency and adaptability in industrial processes.
In practical terms, nanotechnology enables manufacturers to create lighter, stronger, and more multifunctional materials. For instance, nanocoatings can enhance corrosion resistance in industrial machinery, while nanoparticle-infused polymers improve thermal management in electronics. In energy applications, nanostructured catalysts and membranes significantly increase the efficiency of chemical reactions and filtration systems, contributing to sustainability and reduced environmental impact.
Furthermore, in the biomedical sector, nanoscale drug carriers and diagnostic platforms are revolutionizing patient care, offering targeted therapies with minimal side effects. The ability to engineer materials at the nanoscale allows precise control over mechanical, electrical, and chemical properties, opening possibilities that were previously unattainable with conventional materials.
By adopting nanoscale innovations, companies not only achieve superior product performance but also gain a strategic advantage in increasingly competitive global markets. As research advances and production techniques mature, nanotechnology will continue to be a driving force for industrial transformation, bridging the gap between scientific discovery and real-world applications. Harnessing nanotechnology today lays the foundation for the next era of innovation, sustainability, and technological leadership.Harnessing nanotechnology today lays the foundation for the next era of innovation, sustainability, and technological leadership. As industries worldwide adopt nanoscale materials, the pace of innovation is accelerating, paving the way for smarter, greener, and more efficient solutions across all sectors.
To explore how nanomaterials can drive innovation in your products, contact theSuzhou MaxNano Advanced Materials team.